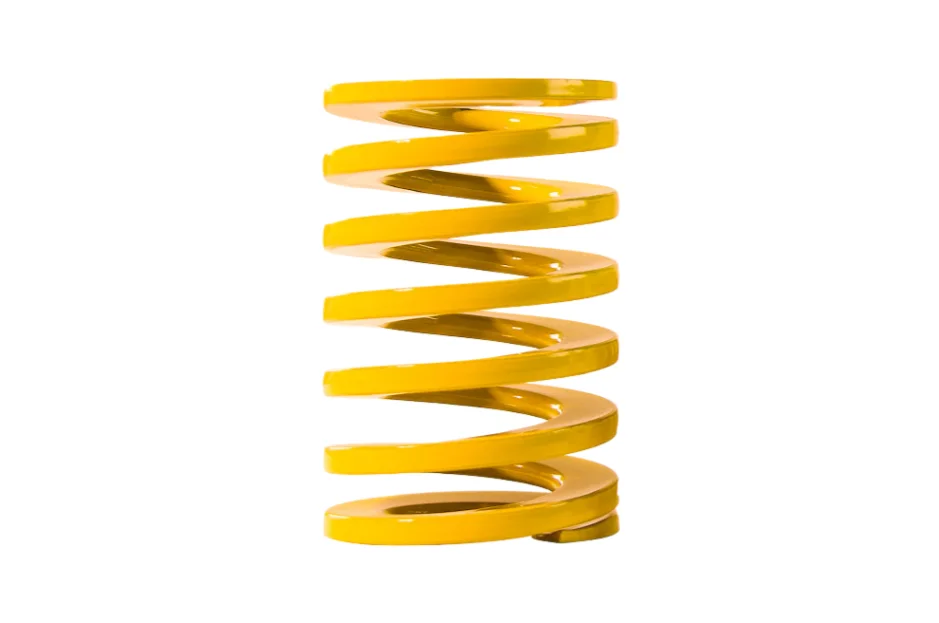
Extra Light Load Yellow Series (1L / Yellow)
Conforming to ISO 10243 specifications with up to 50% maximum deflection. Ideal for long-stroke, light-pressure stamping, electronics hardware dies, and return mechanisms.
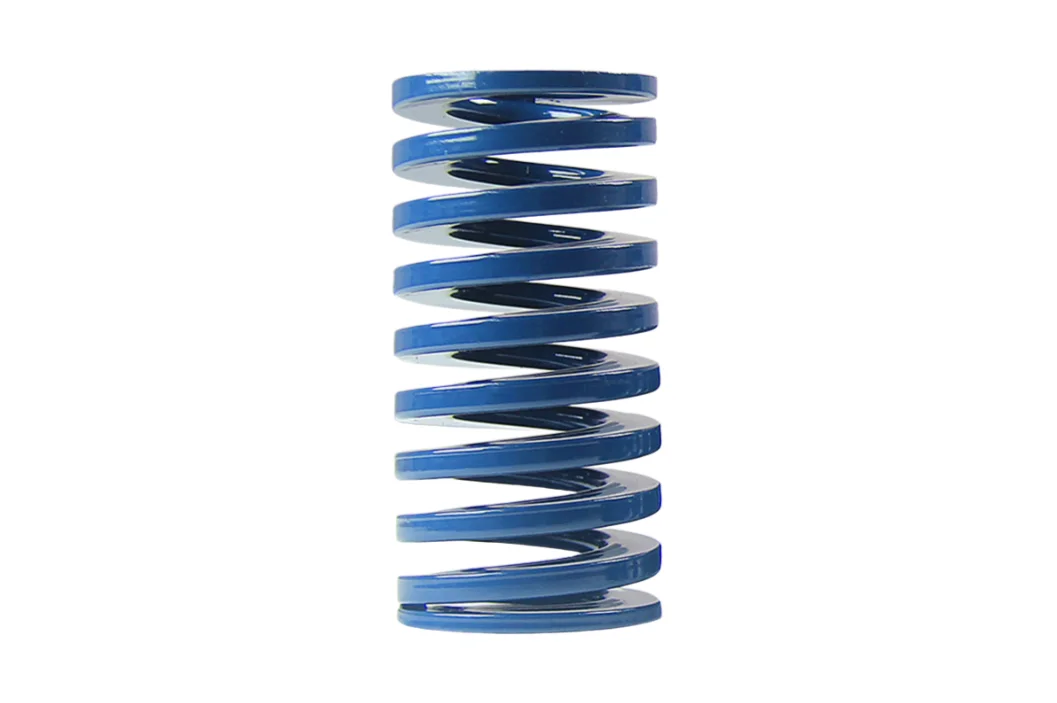
Strictly engineered to ISO 10243 international standards. Cold-coiled from specialized trapezoidal pre-deformed wire, providing over 50% higher energy density than round wire springs. Five standardized color-coded load classes (Yellow, Blue, Red, Green, Brown) for high-speed stamping and injection mold tooling.
Standard round wire springs leave large gaps inside cylindrical pockets, reducing energy density while severe inner-edge stress concentrations lead to early fatigue fractures. Discover why TOSTA rectangular die springs are the choice of toolmakers.
| Evaluation Dimension | TOSTA ISO 10243 Rectangular Die Springs | Standard Round Wire Compression Springs |
|---|---|---|
| Cross-Section Space & EnergyDie Springs | Rectangular cross-section tightly fills cylindrical holes, yielding 45%~60% more energy storage than round wire springs. | Round wire profile leaves large empty gaps between adjacent coils, resulting in poor volumetric energy density. |
| Die Shut Height & Pocket DepthDie Springs | Significantly shorter free length for identical force and travel; cuts machined die shoe pocket depths by 30%~40%. | Demands deep pockets and massive spring banks, making stamping tools excessively tall, heavy, and costly to machine. |
| Inner Edge Stress ConcentrationDie Springs | Cold-coiled trapezoidal pre-deformed wire with radius corners eliminates internal shear stress concentrations. | Round wire undergoes intense inner surface tensile compression when tightly wound, creating premature fatigue micro-cracks. |
| ISO 10243 Visual Color CodingISO Colors | Yellow, Blue, Red, Green, and Brown color coding provides instant visual identification, eliminating assembly mix-ups. | Lacks standardized load color coding; production floor mix-ups between spring stiffness rates frequently cause tool breakage. |
| Epoxy Coating & Oil ResistanceDie Springs | High-adhesion electrostatic epoxy powder coating withstands heavy press impacts, stamping oils, and temperatures up to 200°C. | Ordinary black oxide or electroplating chips off easily under impact; acid pickling poses dangerous hydrogen embrittlement risks. |
| End Squareness & Anti-BucklingDie Springs | Precision ground closed ends with perpendicularity ≤ 1.0°, ensuring true axial compression without lateral buckling or hole scuffing. | Rough or unground wire ends create lateral eccentric moments, causing the spring to bow and gall against mounting hole walls. |
| High-Speed Press Fatigue LifeDie Springs | Undergoes 3x 100% solid pre-setting passes and deep shot peening, delivering 1,000,000 to 3,000,000 high-speed press strokes. | Standard commercial coil springs without deep pre-setting suffer early fatigue fracture within 200,000 to 300,000 cycles. |
Rectangular profile fills the cylindrical mounting pocket tightly, delivering over 50% more force and cutting die shoe pocket depths by 30%~40%.
Five-tier international standard load color coding provides visual assembly verification, preventing tooling mix-ups and catastrophic die crashes.
Precision rolled radius corners on the wire profile disperse flexural shear stress, eliminating stress concentrations along the inner diameter.
Dual ends precision ground to perpendicularity ≤ 1.0°, ensuring perfect axial load alignment and eliminating lateral buckling or pocket wall scuffing.
Fully conforming to ISO 10243 standards across Yellow (1L), Blue (2L), Red (3M), Green (4H), and Brown (5EH) load ratings
Conforming to ISO 10243 specifications with up to 50% maximum deflection. Ideal for long-stroke, light-pressure stamping, electronics hardware dies, and return mechanisms.
The most universally applied die spring worldwide, with 40% maximum deflection. Widely utilized in automotive stamping strippers, progressive dies, and pressure plates.
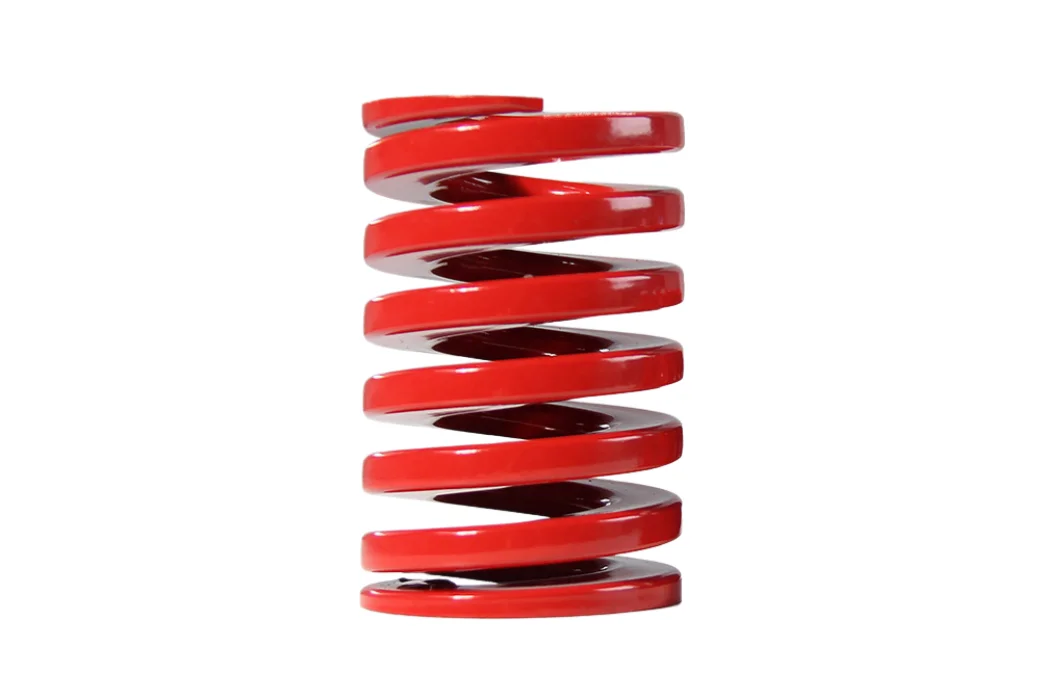
High-stiffness die spring offering up to 32% maximum deflection, engineered for heavy gauge sheet blanking, bending tools, and high-frequency stamping press operations.
Engineered to ISO 10243 specifications with up to 24% maximum deflection. Designed for heavy automotive structural steel, high-tensile sheet blanking, and high-tonnage die strippers.
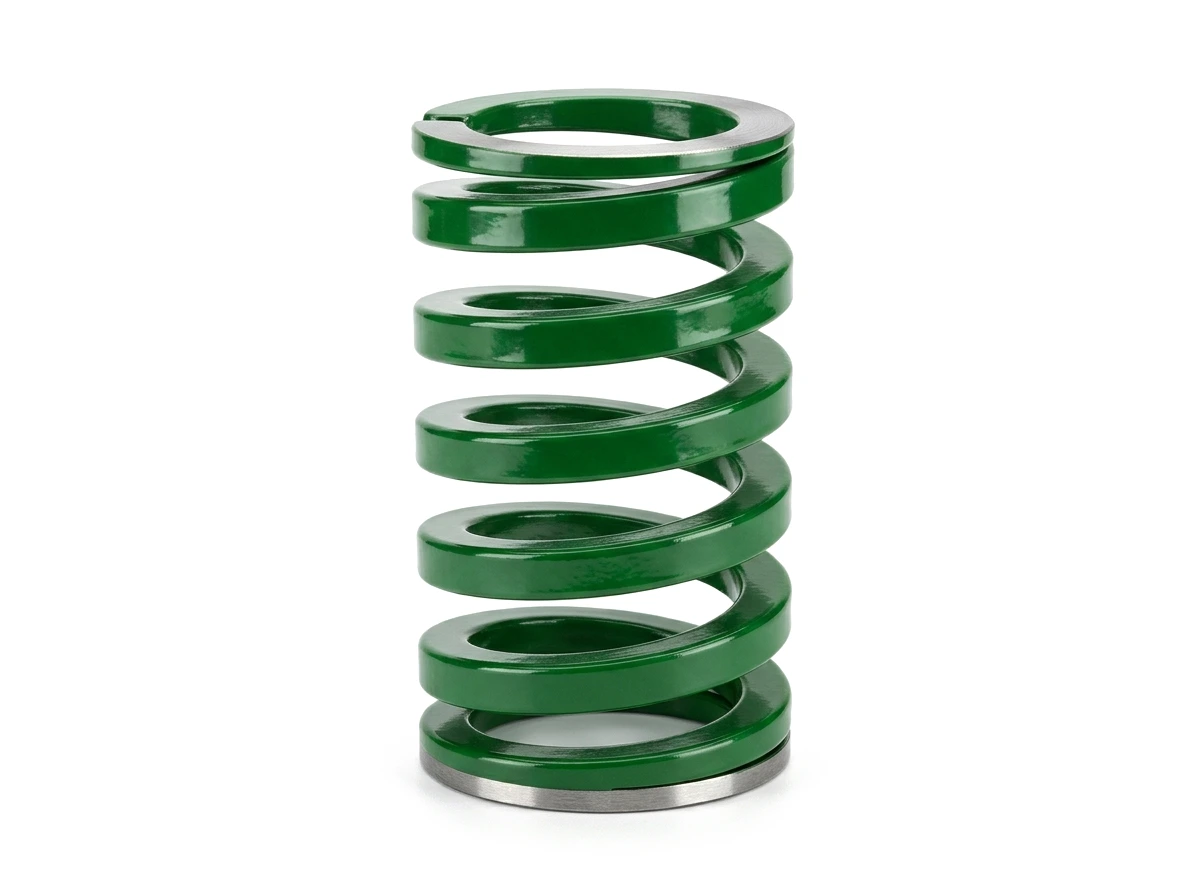
Maximum tonnage die spring class with up to 20% maximum deflection. Built for ultra-high-strength steel (UHSS) cold stamping, heavy bending tools, and large injection mold slide returns.
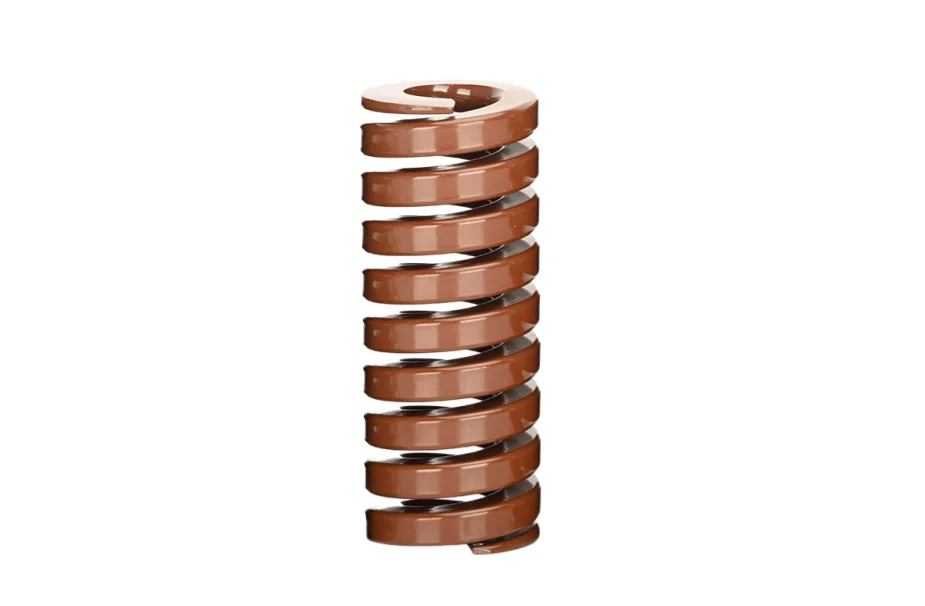
Outer diameters from 10mm to 63mm, lengths from 25mm to 305mm, coiled from high-grade silicon-chrome spring steel (55CrSi / 50CrV4)
| Standard Code | Color Class | Outer Dia. D (mm) | Hole Dia. d (mm) | Free Length L₀ (mm) | Spring Rate k (N/mm) | Max Deflection (mm) | Max Load Fmax (N) |
|---|---|---|---|---|---|---|---|
| 1L 25-050 | Yellow (Extra Light) | 25.0 | 12.5 | 50.0 | 28.5 | 25.0 | 712 |
| 1L 32-075 | Yellow (Extra Light) | 32.0 | 16.0 | 75.0 | 45.0 | 37.5 | 1,687 |
| 1L 40-100 | Yellow (Extra Light) | 40.0 | 20.0 | 100.0 | 68.0 | 50.0 | 3,400 |
| 2L 25-050 | Blue (Light) | 25.0 | 12.5 | 50.0 | 52.0 | 20.0 | 1,040 |
| 2L 32-075 | Blue (Light) | 32.0 | 16.0 | 75.0 | 82.5 | 30.0 | 2,475 |
| 2L 40-100 | Blue (Light) | 40.0 | 20.0 | 100.0 | 125.0 | 40.0 | 5,000 |
| 2L 50-125 | Blue (Light) | 50.0 | 25.0 | 125.0 | 192.0 | 50.0 | 9,600 |
Authored by TOSTA Stamping Tooling Specialists: color coding sizing, energy density comparison, and failure prevention guidelines
Rigorous technical analysis of Yellow, Blue, Red, Green, and Brown load ratings and their corresponding maximum deflection percentages (50% to 20%) to prevent over-travel fatigue failure.
Geometric cavity packing analysis: how trapezoidal wire profiles deform into true rectangular cross-sections upon coiling, distributing shear stress uniformly and eliminating inner edge crack initiation.
Field failure case studies: how press ram angular deflection, lack of 10%–15% pre-travel clamping, and un-chamfered pocket edges lead to premature spring failure, and how to engineer preventive fixes.
Why die springs must always maintain initial 10%–15% pre-travel. Guide rod clearance standards and pocket depth tolerances to eliminate lateral buckling and coil scuffing at 300+ SPM.
Precision preloading across automotive stamping presses, progressive metal dies, and plastic injection molds
TOSTA comprehensive precision spring portfolio — combine different spring types to solve complex engineering challenges
Same wave + compact-space story — the preferred substitute when stiffness requirements are lower.
TOSTA · Precision Industrial Springs
The standard solution for high-stiffness scenarios; partially overlapping load ranges make them interchangeable in some applications.
TOSTA · Precision Industrial Springs
Cost-effective for medium-stiffness, long-travel scenarios — an economical alternative to rectangular springs.
TOSTA · Precision Industrial Springs
Ultra-long life with constant force; pair with rectangular springs for heavy die and heavy-duty buffer systems.
TOSTA · Precision Industrial Springs
Provide press cycle rate, working deflection travel, hole diameter, or target stripping tonnage. TOSTA engineers provide sizing sheets and 3D CAD files within 24 hours.